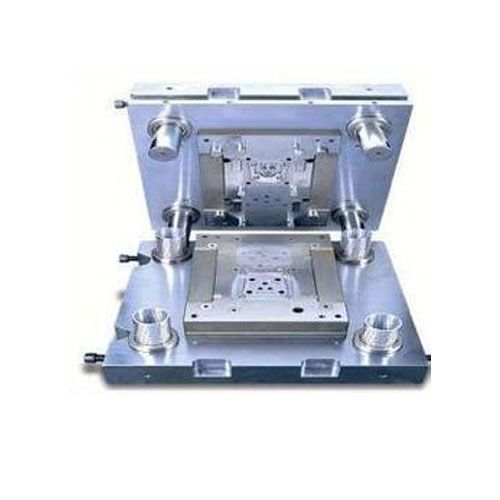
Cold Die Steel is a high carbon steel which relatively lower tungsten, manganese, chromium and molybdenum. These steel grades are used for making cutting tools, sheet metal components, jigs, fixture, Sheering blades & More.
D-2 tool steel is a versatile high-carbon, high-chromium, air-hardening tool steel that is characterized by a relatively high attainable hardness and numerous, large, chromium rich alloy carbides in the microstructure. These carbides provide good resistance to wear from sliding contact with other metals and abrasive materials. Although other steels with improved toughness or improved wear resistance are available, D-2 provides an effective combination of wear resistance and toughness, tool performance, price, and a wide variety of product forms.
| C | CO | CR | MN | MO | NI | P | S | SI | V | W |
|---|---|---|---|---|---|---|---|---|---|---|
| 1.40 – 1.60 | 11.00 – 13.00 | 0.10 – 0.60 | 0.70 – 1.20 | 0.10 – 0.60 | 0.50 – 1.10 |
Flats • Metric • Non-Standard • Rounds • Squares • Standard
| Blanking Dies | Burnishing Tools | Coining Dies |
| Drawing Dies | Extrusion Dies | Forming Rolls |
| Gauges | Knurls | Lamination Dies |
| Lathe Centers | Master Parts | Punches |
| Seaming Rolls | Shear Blades | Slitters |
| Swaging Dies | Threaded Rolling Dies | Trimming Dies |
| Treatment | Temperature Range | Cooling/Quenching | Notes |
|---|---|---|---|
| Forging | 2000-2100° F | Slow. | Heat slowly and uniformly. Do not forge below 1700°F. Cool in vermiculite or other insulating media. |
| Annealing | 1545-1600° F | Cool slowly at a rate of 25° F per hour to 1000° F. | Protect against surface decarburization using controlled atmosphere or by pack-annealing. |
| Stress Relieving | 1020-1200° F | Cool slowly in furnace to 930° F. Then in air. | Stress relieve after rough machining |
| Preheating | 1450-1500° F | Preheat time in furnace is ¾ Hr. per inch of thickness. Heating up to temperature as slow as possible | |
| Hardening | 1800-1900° F | In air. | Temper immediately after hardening. Allow to cool to 125-150° F before tempering. Soak time is 15 minutes per inch of thickness. Minimum of 30 minutes. |
| Tempering | (See Chart) | Complete equalization of temperature throughout the tool is essential for good results. Double temper. Recommended temperature is 400-1000° F |
| Material | Chemistry | Application | |||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| AISI/ASTM | EN | DIN | JIS | C | S | P | SI | Mn | Cr | V | W | Mo | |
| D2 | X155Cr Vmo V12.1 | 1.2379 | SKD11 | 1.45-1.60 | ≤0.03 | ≤0.03 | 0.10-0.60 | 0.20 - 0.60 | 11.00 - 13.00 | 0.70 - 1.00 | 0.90 | Shear blades, blanking punches, die chasers, rolls for cold mills treading rolls and chasers, molds for plastic materials. | |
| D3 | X210Cr12 | 1.2080 | SKD1 | 1.90 - 2.20 | ≤0.02 | ≤0.03 | 0.10 - 0.40 | 0.15 - 0.45 | 11.00 - 12.00 | Rolls for cold strip mills and wire squeezer mills, dies for small metal parts, punching and drawing dies for sinterings. | |||
| A2 | 100CrMoV5-1 | 1.2363 | SKD12 | 1.05 - 1.90 | ≤0.35 | ≤0.35 | 0.20 - 0.40 | 0.40 - 0.70 | 4.80 - 5.01 | 0.10 - 0.30 | 0.40 - 0.70 | Blanking dies, rolls, stamping dies etc. | |
| O1 | 100MNCrW4 | 1.2510 | SKS3 | 0.90 - 1.05 | 1.00 - 1.20 | 0.5 - 0.79 | 0.5 - 0.70 | 0.40 - 0.60 | Dies, blanking punches, moulds for plastic materials. | ||||
| DC-53 | 0.93 | ≤0.010 | ≤0.03 | 0.95 | 0.4 | 7.8 | 0.25 | 1.9 | threading rolls and dies, icy trimming, cutting, stamping tools, precision punching and cutting | ||||