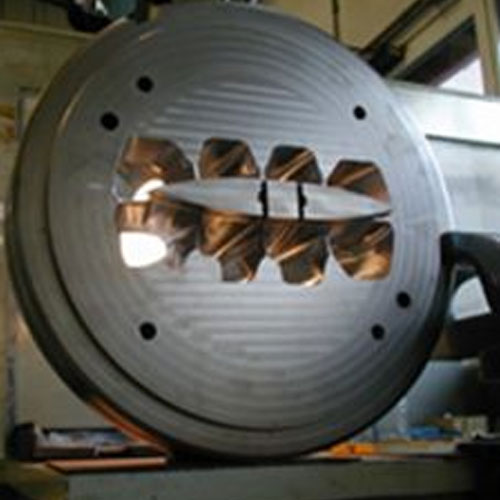
H-13 is an air hardening, 5% chromium die steel, which is an excellent choice for a wide range of hot work and cold work applications. H-13 is widely used for aluminum, zinc, and magnesium die casting dies where resistance to thermal fatigue due to alternated heating and cooling cycles is of primary importance.
Hot Die steel has excellent toughness and resistance to softening under high temperatures, this steel is used in hot work/warm work forging, die casting, and more recently, in hot stamping molds.
| C | CO | CR | MN | MO | NI | P | S | SI | V | W |
|---|---|---|---|---|---|---|---|---|---|---|
| 0.32 – 0.45 | 4.75 – 5.50 | 0.20 – 0.60 | 1.10 – 1.75 | 0.80 – 1.25 | 0.80 – 1.20 |
Flats • Hollowbar • Metric • Non-Standard • Rounds • Squares • Standard
| Die Casting Dies | Dummy Blocks | Extrusion Dies – Hot |
| Forging Dies | Heading Dies – Hot | Heavy Shear Blades |
| Inserts | Mandrels | Piercing Tools – Hot |
| Plastic Mold Dies | Punches – Hot | Swaging Dies – Hot |
| Treatment | Temperature Range | Cooling/Quenching | Notes |
|---|---|---|---|
| Forging | 2000-2100° F | Slow | Do not forge below 1650° F. Anneal after forging. |
| Annealing | 1560-1625° F | Cool slowly at a rate of 35° F per hour to a 1110° F. | Protect against surface decarburization using controlled atmosphere or by pack-annealing. Hold at temperature for 2 hours. |
| Stress Relieving | 1110-1300° F | Cool slowly in furnace to 930° F. Then in air. | |
| Preheating | 1400-1500° F | Preheat time in furnace is ¾ Hr. per inch of thickness. Heating up to temperature as slow as possible. | |
| Hardening | 1830-1900° F | To minimize distortion, air cool. For maximum hardness diameters greater than 6 should be quenched in oil. | Soak time is 30 minutes per inch of thickness. Minimum of 1 hour. Allow to cool to 125-150° F before tempering |
| Tempering | (See Chart) | In air. | Complete equalization of temperature throughout the tools is essential for good results. Double temper. Recommended temperature is 1000-1200° F. |
| Material | Chemistry | Application | |||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| AISI/ASTM | EN | DIN | JIS | C | S | P | SI | Mn | Cr | V | W | Mo | |
| H11 | X38CrMoV5-1 | 1.2343 | 0.33 - 0.41 | ≤0.03 | ≤0.03 | 0.80 - 1.20 | 0.20 - 0.50 | 4.80 - 5.50 | 1.10 - 1.50 | Dies for pressure casting of light alloys, dies for presses for hot forming steel, brass, aluminium and its alloys, hot work shear blades. | |||
| H11M | 0.47-0.52 | ≤0.03 | ≤0.03 | 0.80 -1.20 | 0.20 - 0.50 | 4.80 - 5.50 | 1.10 - 1.50 | Pressure Casting dies, Extrusions tools, Forging, hot shear blades, Screws and barrels | |||||
| H13 | X40CrMoV5-1 | 1.2344 | SKD61 | 0.35 - 0.42 | ≤0.03 | 0.03 | 0.80 - 1.20 | 0.25 - 0.50 | 4.80 - 5.50 | 0.85 - 1.15 | 1.20 - 1.50 | Dies for pressure casting of light alloys, dies for aluminium extrusion dies for hot forming of steels, extractors. | |
| H13M | 0.47 - 0.52 | ≤0.03 | ≤0.03 | 0.80 - 1.20 | 0.25 - 0.50 | 4.80 - 5.50 | 0.85 - 1.15 | 1.20 - 1.50 | Dies for pressure casting of light alloys, dies for aluminium extrusion dies for hot forming of steels, extractors. | ||||
| TGE-13 | 0.38 | ≤0.002 | ≤0.015 | 0.9 | 0.35 | 5 | 0.95 | 1.35 | metal pressure die casting, hot extrusion moulds, plastic moulds, | ||||
| TGGP-13 | 0.39 | ≤0.001 | ≤0.009 | 1.1 | 0.4 | 5.3 | 1 | 1.45 | Alloy die casting mould, hot extrusion moulds, precise hot forging moulds, | ||||
| TGE-23 | 0.37 | ≤0.001 | ≤0.015 | 0.3 | 0.4 | 5 | 0.45 | 2.2 | Pressure die casting, extrursion molds, forged molds and inserts | ||||
| TG-1.2367 | 0.37 | ≤0.001 | ≤0.015 | 0.4 | 0.45 | 5 | 0.55 | 2.8 | Pressure die casting, extrursion molds, moulded trimming dies, compression moulding inserts, hot shearing blades | ||||